A lot has changed since our earliest days in food manufacturing.
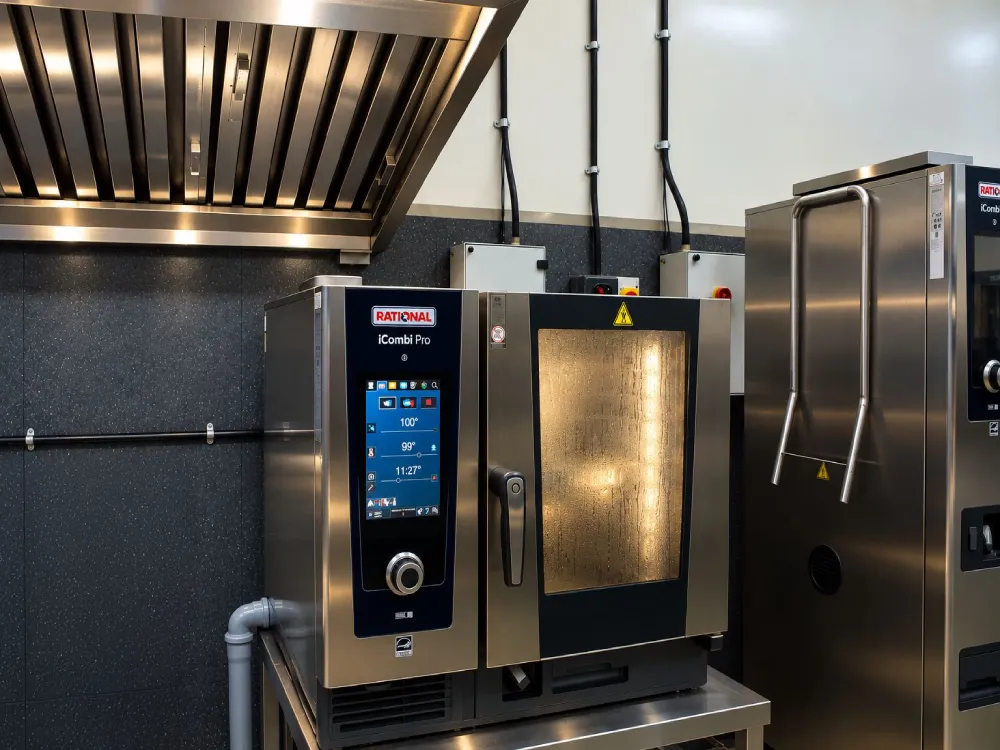
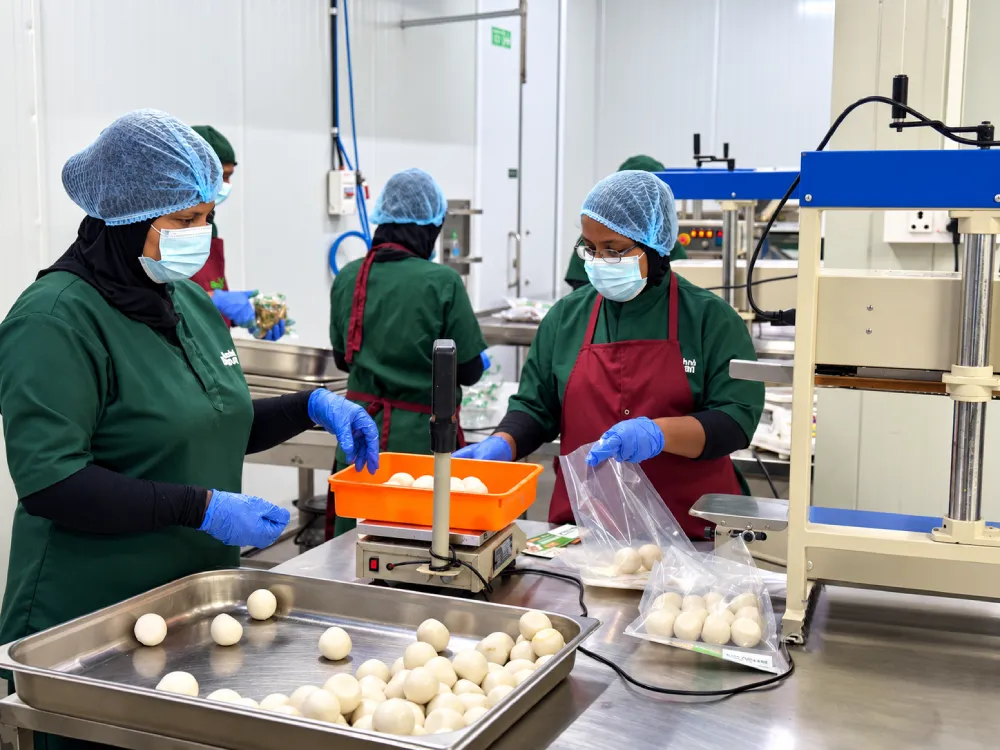
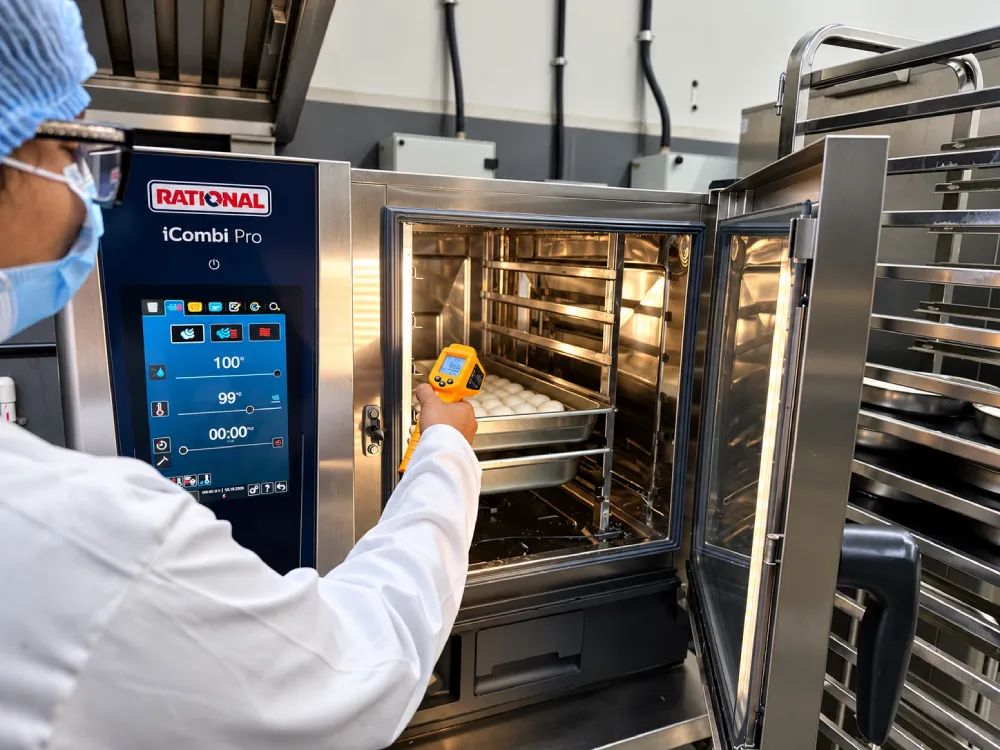
Today, sophisticated machinery, controlled processes and modern packaging systems allow us to manufacture at a scale that would have been difficult to imagine when the journey began
But machines alone
don't make good food.
It takes the right ingredients.
The right process.
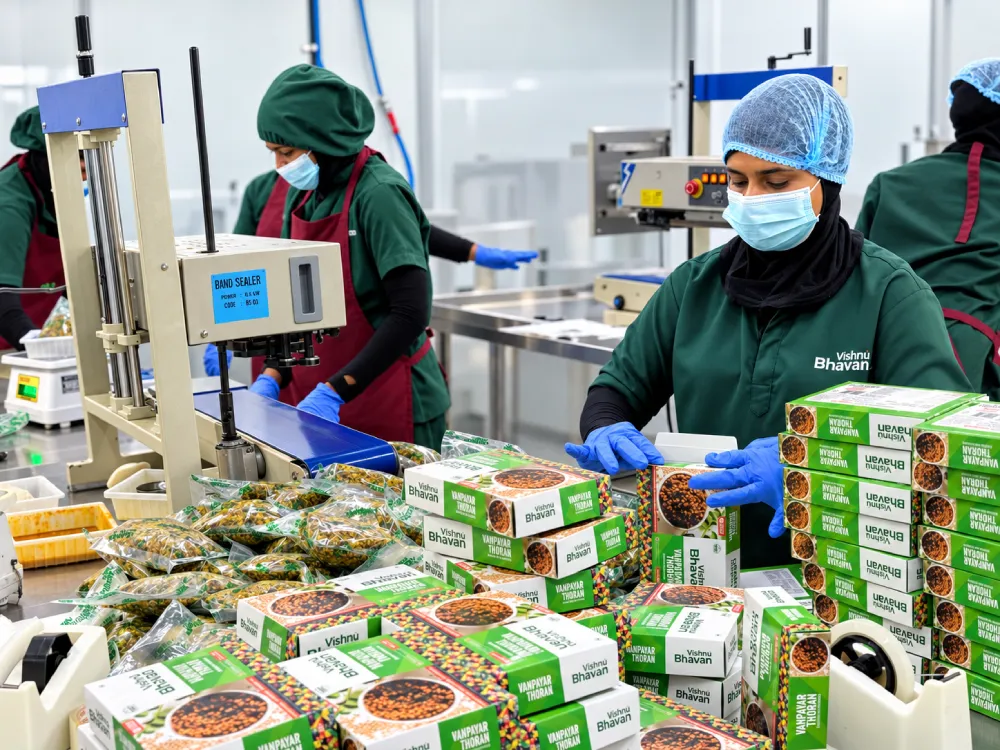
People who understand what they are doing
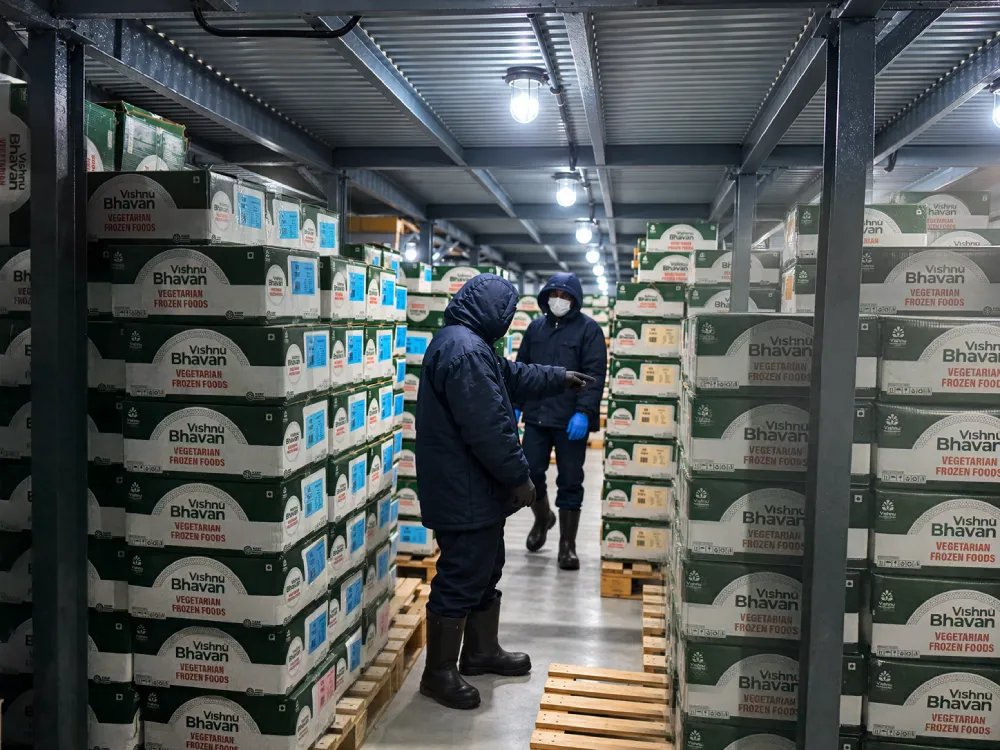
And systems that make sure the same standards are followed every time.
Our manufacturing infrastructure has been developed around that philosophy.
Our Manufacturing Capabilities
Built to Handle Scale Without Losing Control
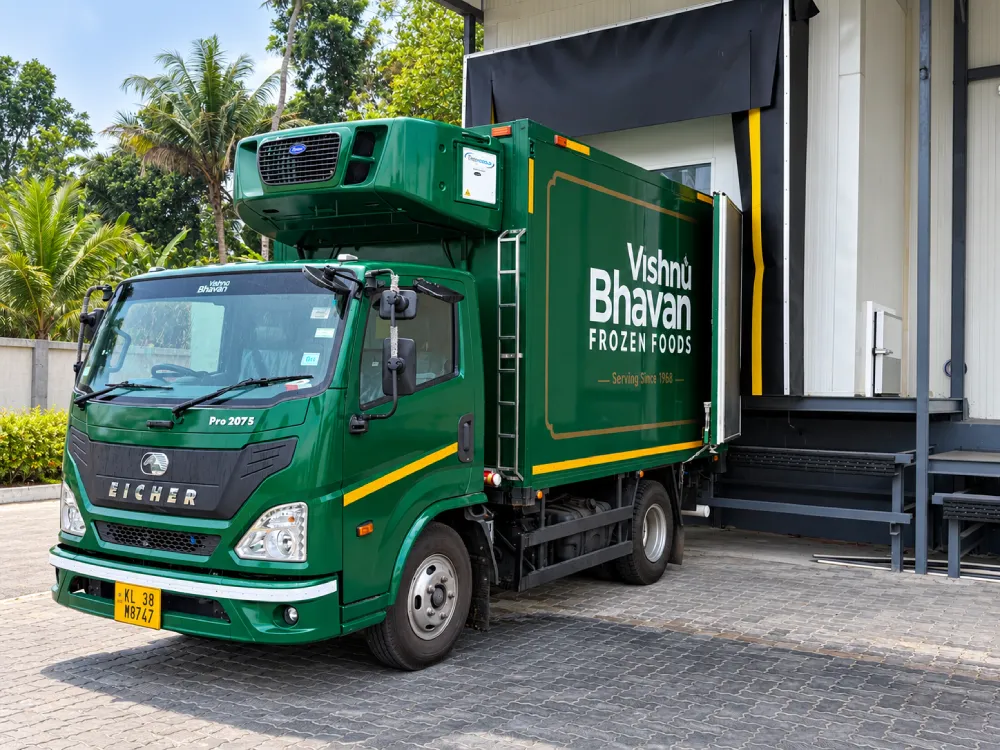
Today our manufacturing capabilities include:
650
Tonnes
Approximate annual production capacity.
10+
Varieties
Across multiple food categories.
70+
Products
Handled across our daily manufacturing portfolio.
Multiple Global Markets
Supported through manufacturing capabilities developed for domestic and international requirements.
The scale is important. But consistency at that scale matters more.
WHAT WE MANUFACTURE
Different Products. One Responsibility.
Every food category behaves differently.
Spices need their aroma protected.
Blends demand precision.
Rice and cereals require careful handling.
Oils require appropriate processing and packaging controls.
That is why our manufacturing capabilities have developed across specialised food categories rather than around a single production process